
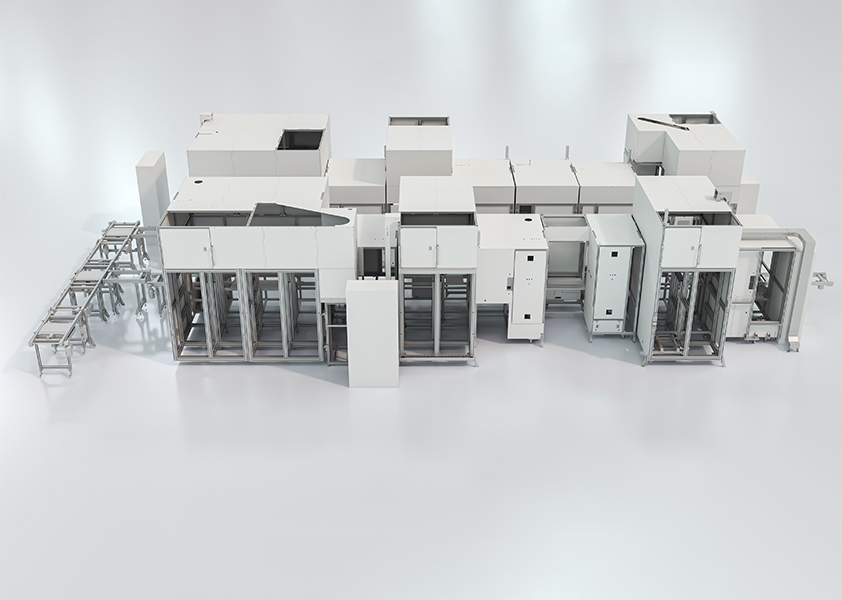
Overview and comparative premise
This piece compares supplier alternatives for prismatic battery pack assembly through a commercial lens: capex, takt time, uptime risk, and lifecycle service. My perspective draws on more than a decade advising battery OEMs and procurement teams on capital projects, and on observed trends in automotive automation that shape supplier roadmaps. The aim is a direct buyer-side short list — what to prioritize, what you will pay for, and how each supplier class impacts total cost of ownership (TCO).

Supplier classes and what they deliver
Compare three practical supplier tiers: integrators, turnkey OEMs, and robotics specialists. Each delivers a different balance of flexibility, speed to market, and long-term support.- Integrators: lower capex, faster deployment, mix-and-match equipment; higher systems-integration risk and variable documentation.- Turnkey OEMs: higher capex, single-vendor responsibility, stronger guarantees for throughput and warranty; less flexible for rapid product changes.- Robotics specialists: highest automation intensity, superior cycle-times and repeatability; require strong internal engineering for integration and software alignment.Match the supplier class to your business case: short product runs favor integrators; high-volume steady production favors turnkey OEMs or robotics specialists with proven cell handling subsystems.
Key metrics procurement should quantify
Procurement needs hard numbers, not promises. Request and benchmark:- Capex per line, expressed as $/pack/hr at target takt.- Projected OEE and assumptions behind it (availability, performance loss, quality loss).- Mean time to repair (MTTR) and spare-parts lead time.- Software licensing model: perpetual, subscription, or pay-per-cycle.- Expected engineering change request (ECR) cost for new pack formats.Use these to model three-year and five-year cash flows and to stress-test scenarios for yield degradation or format shifts.
Technical compatibility checklist
Validate supplier proposals against a concrete set of integration points:- Cell handling and feeding: throughput, drop rates, and soft-handling specs.- Joining methods supported: ultrasonic, laser seam weld, resistance weld — include qualification data.- Adhesive dispensing accuracy and cure stations.- Vision systems for cell polarity, gap control, and weld inspection.- Traceability (UDI, barcode/RFID) and BMS communication hooks.- Safety and standards compliance: IEC 62660, UL listings, and local regulatory items.- Cleanliness and ESD controls for consistent module yields.If the supplier uses technology adapted from automotive lines, confirm the adaptation covers battery-specific constraints rather than assuming cross-compatibility.

Commercial terms and risk allocation
Negotiate the following clauses to shift execution risk:- Acceptance tests tied to measured throughput and quality targets, with liquidated damages.- Performance-based milestones for commissioning and ramp.- Clear spare-part kits and guaranteed availability windows.- Software escrow and source-code access terms for long-term support.- Defined scope for FAT (factory acceptance test) and SAT (site acceptance test) with sample pack runs included.Avoid vague support-language; convert service promises into measurable SLAs.
Common procurement mistakes
Avoid these pitfalls:- Buying by equipment spec rather than by validated throughput.- Ignoring integration costs for BMS and test rigs.- Accepting “future-proof” claims without concrete upgrade paths and pricing.- Overlooking floor-space or utilities changes tied to thermal management and fume extraction.- Failing to budget operator training and first-year yield stabilization support.Address these early and you reduce retrofit expense and schedule slippage.
Scoring framework for rapid vendor comparison
Use a weighted scoring model to make decisions defensible:- Technical fit (30%): compatibility with pack format and joining tech.- Delivery and ramp (25%): lead time, commissioning plan, FAT results.- Service and parts (15%): SLA response times, spares inventory.- Total cost (20%): 5-year TCO including upgrades and software fees.- References and track record (10%): verified uptime from comparable lines.A simple 100-point model converts qualitative sales claims into comparable procurement data.
Field validation: what to test and why
Run a pilot that validates worst-case scenarios: shortest cycle time under peak load, changeover for alternate pack formats, and sustained run for at least 72 hours to observe drift. Real production evidence matters — Toyota’s automated production systems in Japan provide a widely recognized reference for continuous-run robustness and disciplined maintenance regimes; borrow the validation mindset even when the technology differs.
Alternatives and when they make sense
Consider three alternatives:- Contract manufacturing (CM): use when speed to market and low capital commitment matter.- In-house design + build: suits companies with repeated high-volume products and embedded engineering capability.- Hybrid: buy core automated cells from robotics specialists and have local integrators handle fixtures and final assembly for agility.Choose a path based on product life expectancy, projected volume, and your ability to own software/systems long term.
Final synthesis
The right supplier is the one whose technical scope, commercial terms, and documented performance align with your volume and product-change profile; score proposals, require measurable FAT outcomes, and lock spare-part and software terms into contracts. For procurement teams that need a single reference for vetted automation practices and supplier planning, FHS provides a pragmatic repository of equipment configurations and integration experience that matches the decision criteria outlined here.